中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
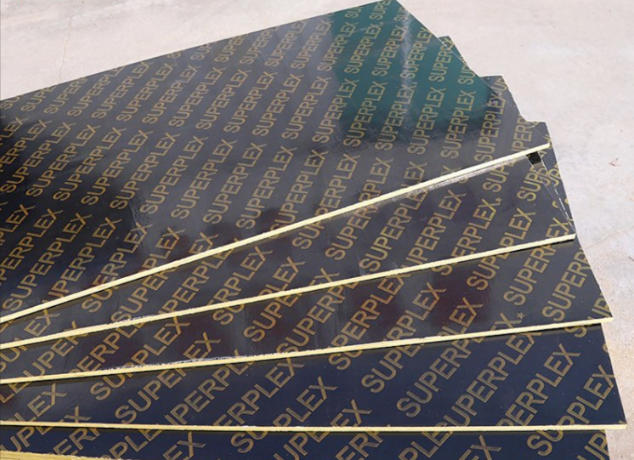
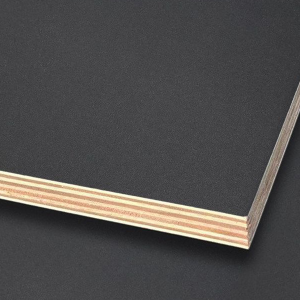
Sourcing film faced plywood (formwork plywood) carries three main risks: insufficient reuse cycles, batch-to-batch quality variation, and poor matching between film and substrate. In recent years, PVC film faced plywood has become more common. Quality products can achieve over 20 reuses, but process capability varies widely between suppliers. This guide provides a structured evaluation framework to help international buyers systematically screen reliable suppliers.
1. Technical Parameters to Confirm Before Purchasing
Clarify the following parameters before requesting quotes. Without them, quotations are not comparable.
| Parameter | Options | Notes |
|---|---|---|
| Film type | Phenolic film / PVC film | PVC film can exceed 20 reuses; verify film adhesion |
| Reuse cycles required | 10 / 20 / 30 | Directly determines core density, glue type, and film weight |
| Thickness | 12mm / 15mm / 18mm / 20mm | 18–20mm common for high-rise buildings |
| Core | Poplar / Eucalyptus / Birch | Eucalyptus and birch are better for high reuse |
| Glue type | MR / WBP | WBP phenolic glue resists boiling, suitable for humid environments |
| Film color | Black / Brown / Red | Color does not affect performance, but batches must be consistent |
| Size | 1220×2440mm / custom | Confirm whether customization is available |
2. Five Core Dimensions for Supplier Evaluation
1. Production Equipment and Film Lamination Capability
Press tonnage and hot platen size: determine core density uniformity
Sanding line precision: affects substrate flatness and film lamination
Lamination line: whether there is an independent lamination line, especially for PVC
Hot pressing parameters: stability of temperature, pressure, and time
2. Raw Material Control
Veneer grade and repair rate
Glue brand and type (MR or WBP)
Film source and weight (phenolic film generally ≥120 g/m²)
PVC film thickness and adhesion
3. Laboratory and Testing Capability
Bonding strength testing machine
Moisture content meter
Film adhesion testing equipment
Density and thickness tolerance testing
4. Batch Stability
Batch records kept
Test data for consecutive batches available
Third-party inspection accepted
5. Export Experience and After-Sales Policy
Export experience in your target market
Quality complaint handling process
Commitment on reuse cycles
Compensation for non-conformity and coverage of replacement shipping
3. Standard Sample Testing Procedure
Sample testing is a key step in supplier screening. Follow these steps:
Boiling test: 72-hour boiling, observe edge delamination.
Repeated bending test: check film cracking and whitening (especially PVC).
Hard object scratch test: evaluate film wear resistance.
On-site reuse test: small batch on site, record actual reuse cycles.
Thickness and flatness check: use caliper and straightedge to check thickness tolerance and surface waves.
Samples must match bulk production. If samples pass but bulk does not, it is a supplier breach.
4. Factory Audit Checklist
A factory audit should not be limited to the showroom. Focus on:
| Area | Check Points |
|---|---|
| Production line | Press tonnage, hot platen size, sanding line, lamination line |
| Warehouse | Raw material brand, grade, storage conditions |
| Laboratory | Testing equipment, batch records, test reports |
| Semi-finished area | Veneer repair, glue spread uniformity |
| Finished product area | Film adhesion, surface flatness, thickness tolerance |
Questions to Ask:
What core density do you control?
What is the thickness tolerance?
What is the film type and weight?
Is the glue MR or WBP?
Can PVC film guarantee over 20 reuses?
Do you accept third-party inspection?
5. Key Contract Clauses
The contract should specify:
Thickness tolerance (standard ±0.5mm, high requirement ±0.3mm)
Surface flatness standard
Film type and weight
Glue type (MR or WBP)
Reuse cycle commitment (e.g., PVC ≥20)
Compensation method for non-conformity
Responsibility for replacement shipping
Delivery time and delay liability
Suppliers with vague after-sales policies should not be chosen, even at lower prices.
6. Common Risks and Prevention
| Risk | Prevention |
|---|---|
| Thin film sold as thick | Request weight test report |
| Poor PVC film, whitens when bent | Repeated bending test on samples |
| Hollow core or rotten poplar | Factory audit: veneer grade and repair |
| MR glue sold as WBP | Request glue type certificate |
| Exaggerated thickness tolerance | Sampling inspection on receipt |
| Exaggerated reuse cycles | Written commitment and compensation clause |
| Samples inconsistent with bulk | Seal samples and compare with bulk |
7. Frequently Asked Questions (FAQ)
Q1: PVC or phenolic film faced plywood — which is better for high-rise buildings?
A: PVC film faced plywood offers a flatter surface, better weather resistance, and over 20 reuses, suitable for high-rise and fair-faced concrete. Phenolic film faced plywood resists alkali and boiling, suitable for humid environments and standard concrete casting. The choice depends on project requirements and budget.
Q2: How to judge PVC film quality?
A: Check film adhesion and bending resistance. Good PVC film does not whiten or delaminate after repeated bending. Poor film whitens at the first bend and peels after a few uses. Test bending on samples.
Q3: What is required to achieve over 20 reuses?
A: High-density core (eucalyptus or birch), WBP phenolic glue, high-quality film (phenolic ≥120 g/m² or premium PVC film), and stable hot pressing process.
Q4: What should be looked at first during a factory audit?
A: The press, sanding line, lamination line, and laboratory. Factories with an independent lamination line are usually more stable.
Q5: What must be written in the contract?
A: Thickness tolerance, film type and weight, glue type, reuse cycle commitment, compensation for non-conformity, replacement shipping, and delivery delay.
Q6: What tests should be done on samples?
A: Boiling, repeated bending, hard object scratching, and on-site reuse. For PVC film, focus on bending whitening and adhesion.
Q7: What are the common traps?
A: Thin film sold as thick, hollow core, MR sold as WBP, exaggerated thickness tolerance, exaggerated reuse cycles, and samples inconsistent with bulk.
Q8: Why is stability more important than low price?
A: A product 10% cheaper but unstable costs far more in rework, claims, and lost customers. Stability means fewer worries and fewer complaints.