中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
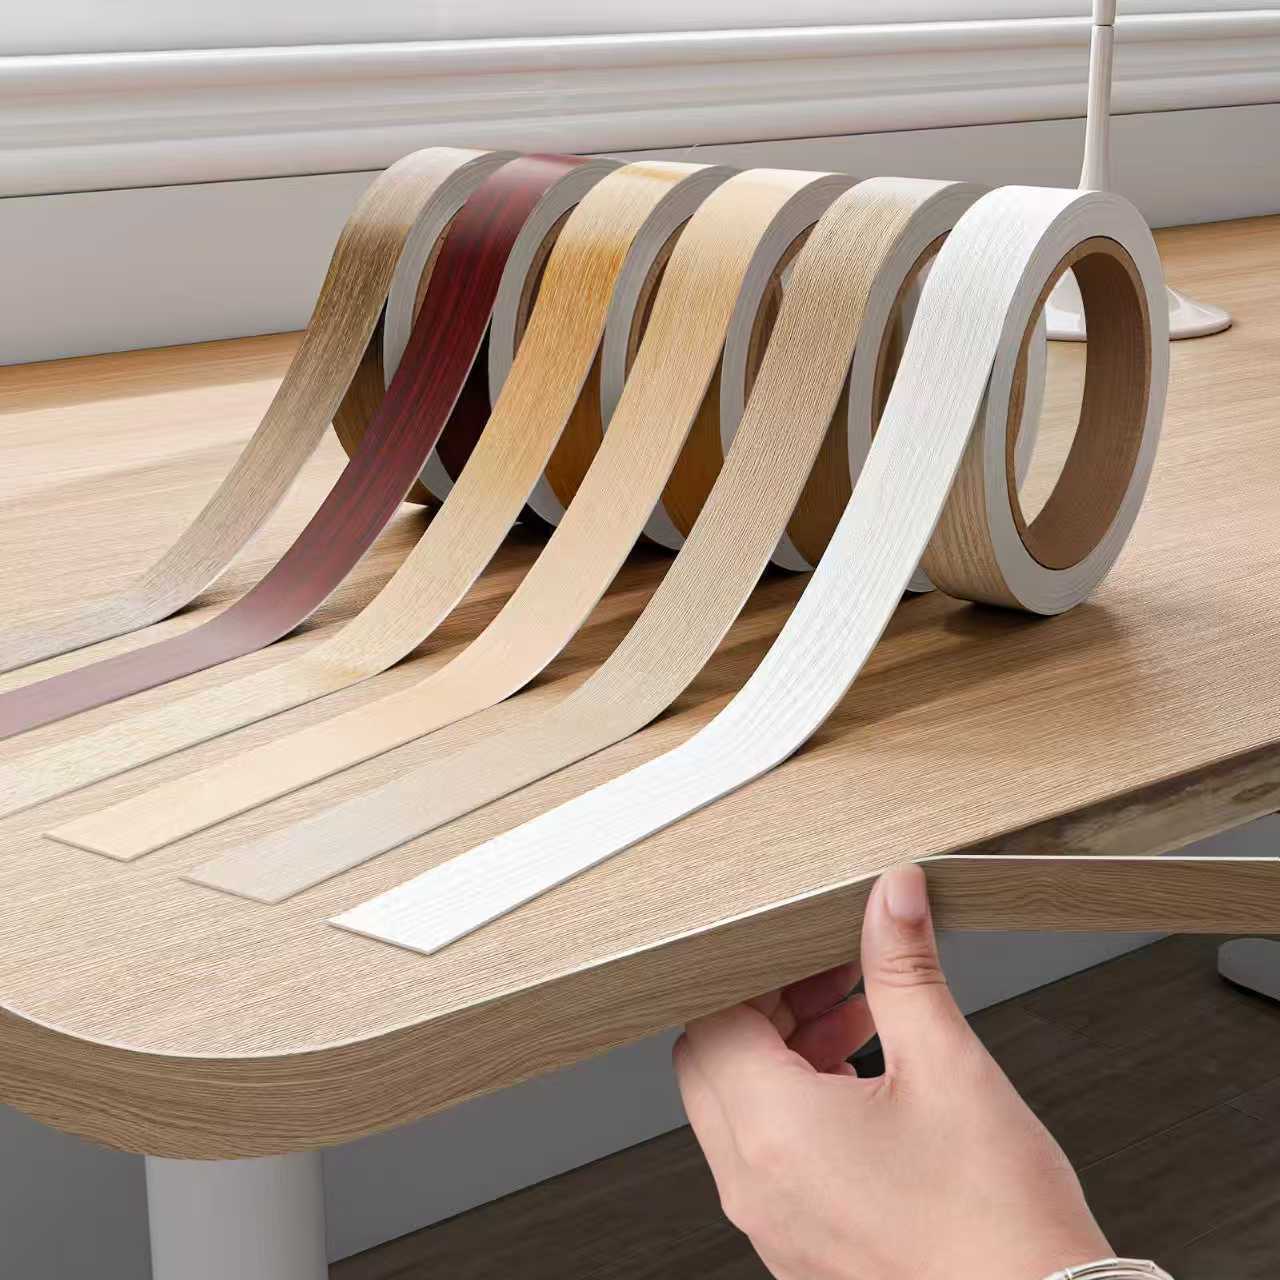
I. Basic Concept of Edge Banding
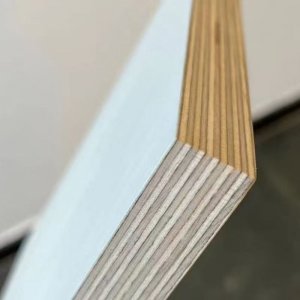
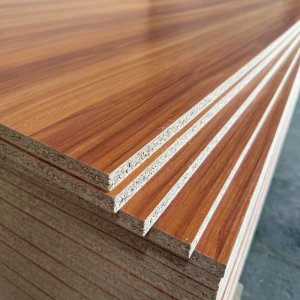
Edge banding (Edge Banding / Edge Tape) is a narrow strip of decorative and protective material applied to the cut edges of wood-based panels such as plywood, particleboard, and medium-density fiberboard (MDF). It is bonded to the panel side with an adhesive (hot-melt glue or solvent-based glue), achieving sealed protection of the panel's internal structure and beautification of its appearance.
In panel furniture and interior decoration, edge banding accounts for only a tiny proportion of material cost (usually less than 3-5%), yet it has a decisive impact on product service life, environmental performance, appearance quality, and safety of use. There is an old saying in the industry: "To judge the quality of a piece of furniture, look first at its edge banding." The quality of edge banding application often directly reflects the technical level of a furniture manufacturer.
The core functions of edge banding can be summarized in four levels:
| Functional Level | Specific Role |
|---|---|
| Physical protection | Seals the cut edge of the panel, blocks the intrusion paths of moisture, dampness, and dust, preventing the substrate from swelling, delaminating, powdering, or molding |
| Environmental sealing | Tightly seals free formaldehyde and VOCs inside the substrate, preventing them from volatilizing into indoor air; an important defense line for indoor air quality |
| Structural reinforcement | Through firm bonding between the edge banding and the panel edge, enhances the edge's impact resistance and wear resistance, preventing corner damage |
| Decorative beautification | Covers the internal layered structure or particle form of the panel, giving the furniture a unified, refined, and premium appearance |
II. Main Types of Edge Banding and Material Characteristics
2.1 Classification by Material
The mainstream edge banding products on the market can be grouped into the following five major categories, each with different performance characteristics and application scenarios:
| Type | Material Composition | Thickness Range | Characteristics | Applications |
|---|---|---|---|---|
| PVC edge banding | Polyvinyl chloride resin + calcium carbonate filler + plasticizer + stabilizer + pigment | 0.4-3.0mm | Economical, good flexibility, rich colors; currently the most mainstream edge banding material | Panel furniture, cabinets, office furniture (general purpose) |
| ABS edge banding | Acrylonitrile-butadiene-styrene copolymer | 0.8-2.0mm | Pure material, rounded and translucent edge after trimming without whitening, premium feel, better weather resistance than PVC | High-end furniture, kitchen & bath, children's furniture, export products |
| Melamine edge banding | Melamine impregnated paper | 0.2-0.8mm | High color matching, good adhesion, stable dimensions under heat and cold, but relatively brittle | Matching edge banding for melamine-faced panels |
| Wood veneer edge banding | Natural wood veneer (oak, walnut, cherry, etc.) | 0.3-0.6mm | Natural and realistic grain, excellent texture, integrates with solid wood veneered furniture | High-end solid wood furniture, natural wood veneer furniture |
| Metal edge banding (aluminum alloy) | Aluminum alloy profile | 1.0-3.0mm | Sturdy and durable, excellent fire and moisture resistance, strong modern feel | Commercial furniture, laboratory furniture, office partitions, kitchen countertops |
2.2 PVC Edge Banding — In-Depth Analysis of the Market Mainstay
PVC edge banding accounts for about 70% of the global edge banding market and is the most widely used edge banding material. Its production processes and quality vary greatly; the performance gap between high-quality PVC edge banding and inferior products can be several times.
Technical Characteristics of High-Quality PVC Edge Banding:
Filler control: Calcium carbonate (CaCO₃) filler content controlled at 15-25%. Too low: high cost and insufficient hardness; too high (inferior products can reach 40-50%): flexibility drops sharply, brittle in winter, edge chipping during trimming.
Plasticizer system: Uses environmentally friendly plasticizers such as DOTP (dioctyl terephthalate) or TOTM (trioctyl trimellitate) to replace traditional phthalate plasticizers such as DEHP and DBP. Eco-friendly plasticizers contain no phthalates and comply with EU REACH and RoHS directives.
Anti-UV additives: UV absorbers and hindered amine light stabilizers (HALS) prevent discoloration and powdering under long-term light exposure, and white edge banding from yellowing.
Wear-resistant layer: High-end PVC edge banding has a transparent wear-resistant layer (PMMA or PU) on the surface, significantly improving scratch resistance, suitable for high-frequency contact surfaces such as desktops and countertop edges.
Key Performance Indicators of PVC Edge Banding:
| Performance Indicator | Test Method | High-Quality Standard | Inferior Performance |
|---|---|---|---|
| Flexibility (cold bend) | Bend 180° at -5°C | No cracks | Breakage or whitening |
| Heat resistance (thermal stability) | 200°C hot press test | No sticking to board, no discoloration | Melting and sticking, severe discoloration |
| Abrasion resistance (Taber) | CS-17 wheel, 500g load | Pattern clear after 500 cycles | Pattern disappears or wears through |
| Color difference (ΔE) | Colorimeter between batches | ΔE≤0.5 (invisible to naked eye) | ΔE≥1.0 (visible color difference) |
| Gloss deviation | Multi-point measurement in same batch | Deviation ≤±3GU | Deviation ≥±8GU |
2.3 ABS Edge Banding — The Quality Choice for the High-End Market
ABS edge banding has risen rapidly in the high-end furniture market in recent years. Its overall performance is superior to PVC, but its price is about 1.5-2.5 times that of PVC.
Core Advantages of ABS Edge Banding:
No whitening after trimming: This is the most distinctive identification feature of ABS edge banding. No matter how sharp the trimming knife is, the cut edge always maintains the material's natural color (black ABS edge is pure black, white ABS edge is pure white), unlike PVC which whitens due to stress. This property gives furniture edges clear, sharp lines and a premium feel.
Excellent weather resistance: The glass transition temperature (Tg) of ABS resin is about 105°C, much higher than PVC's around 80°C. ABS edge banding is more stable in high-temperature environments, less prone to softening and deformation; it maintains good flexibility in low-temperature environments and is less prone to brittle cracking.
Pure material: ABS edge banding contains no filler (or very little special filler), offering good material uniformity, more stable bonding strength after hot-melt adhesive application, and less aging failure of the adhesive layer.
Better environmental performance: ABS itself is non-toxic, odorless, emits less smoke when burned, and does not release corrosive gases such as hydrogen chloride that PVC releases when burned.
2.4 Melamine Edge Banding — The Classic Solution for Matching Colors
Melamine edge banding is a thin edge banding made by printing wood grain or solid-color patterns on melamine impregnated paper, then drying and cutting. It is highly compatible with the synchronous pressing process of melamine-faced panels.
Technical Points:
Thickness is usually 0.2-0.8mm, relatively thin, suitable for tight bonding with faced panels
Surface has a grain-matching design — the edge banding texture aligns continuously with the panel color, visually achieving integration of panel and edge banding ("seamless edge banding" effect)
Bonding method with the panel: EVA hot-melt adhesive or PUR hot-melt adhesive, achieving good bonding strength through low-temperature and low-pressure pressing
Limitations:
Relatively brittle, easily broken when edge banding sharp corners, not suitable for large arcs or irregular edge banding
Impact resistance inferior to PVC and ABS, corners easily damaged after impact
High requirements for application temperature (edge banding machine temperature must be precisely controlled at 160-200°C); overheating or low temperature can cause surface discoloration or poor bonding
III. Quality Standards and Testing Methods for Edge Banding
3.1 Appearance Quality
High-quality edge banding should meet the following appearance requirements:
Smooth and uniform surface: no bubbles, particles, pits, or scratches
Consistent color: color difference ΔE≤0.5 within the same batch, ΔE≤1.0 between batches
Straight edges: no obvious waviness or unevenness on roll edge banding edges, facilitating continuous feeding of automatic edge banding machines
Clear printing: wood grain edge banding has clear texture, accurate registration (deviation ≤0.2mm), no ghosting
3.2 Dimensional Accuracy (LY/T 2383-2014 "Edge Banding for Wood-Based Panel Facing")
| Item | Allowable Deviation |
|---|---|
| Width | ±0.15mm (width ≤50mm); ±0.20mm (width >50mm) |
| Thickness | ±0.03mm (thickness ≤1.0mm); ±0.05mm (thickness >1.0mm) |
| Length | ±3mm/100m |
Dimensional accuracy deviation directly affects the adaptability of the edge banding machine's feed rollers — excessive deviation can cause edge banding to deviate or jam, interrupting continuous edge banding operations.
3.3 Physical and Mechanical Properties
(1)Peel Strength (Bonding Fastness)
This is the core indicator for measuring the bonding fastness between edge banding and substrate. Test method: bond edge banding to standard substrate (particleboard/MDF), peel at 180° angle at constant speed using a peel tester, record peel force.
Qualified standard (LY/T 2383): Peel strength ≥1.5 N/mm
High-quality standard (JINDIWOOD requirement): ≥2.5 N/mm
(2)Cold-Heat Cycle Resistance
Place edge-banded specimens alternately in high temperature (63±3°C) and low temperature (-20±2°C) environments for 2 hours each, cycling 5 times. Observe edge banding for cracking, debonding, discoloration.
(3)Aging Resistance (Xenon Lamp Aging)
Place specimens in a xenon lamp aging test chamber, expose for 500 hours, then measure color difference and peel strength retention. High-quality edge banding should meet:
Color difference ΔE≤2.0
Peel strength retention rate ≥80%
3.4 Environmental and Safety Performance
(1)Heavy Metal Content (PVC Edge Banding)
Since PVC edge banding contains stabilizers (usually calcium-zinc composite stabilizers or organotin stabilizers), heavy metal content must be strictly controlled. Tested according to GB/T 26125 (IEC 62321), it should meet the following limits (RoHS directive requirements):
| Heavy Metal Element | Limit (mg/kg) |
|---|---|
| Lead (Pb) | ≤1000 |
| Mercury (Hg) | ≤1000 |
| Cadmium (Cd) | ≤100 |
| Hexavalent chromium (Cr⁶⁺) | ≤1000 |
| Polybrominated biphenyls (PBB) | ≤1000 |
| Polybrominated diphenyl ethers (PBDE) | ≤1000 |
(2)Phthalate Content (Plasticizers)
Prefer non-phthalate plasticizers such as DOTP, TOTM, DINP. Total phthalate plasticizers (DEHP, DBP, BBP, DIBP) content should be ≤1000mg/kg (compliant with REACH Annex XVII requirements).
(3)VOCs Emission
Edge banding should have no obvious irritating odor during storage and use. Tested according to ISO 16000-6, TVOC emission ≤100μg/m³.
IV. Edge Banding Production Processes
4.1 PVC/ABS Edge Banding Production Process
Step 1: Batching and Mixing
PVC resin powder, plasticizer, stabilizer, filler, pigment, anti-UV additives, etc. weighed according to formula
Put into high-speed mixer for mixing (temperature 80-120°C) to uniformly disperse all components
Cool to room temperature and transfer to storage hopper for later use
Step 2: Extrusion Molding
Mixed material is heated and plasticized through single-screw or twin-screw extruder (barrel temperature 160-200°C, temperature gradient control in different zones)
Molten material is extruded into thin sheet through T-die, thickness controlled jointly by die opening and extrusion speed
Thin sheet is calendered and shaped by three-roll calender (upper, middle, lower rolls, temperature controlled at 120-150°C) to obtain precise thickness and smooth surface
Step 3: Surface Treatment (Printing and Texturing)
Printing layer (wood grain or color): Gravure printing or flexographic printing transfers the pattern to the edge banding surface, using special ink, registration accuracy ≤0.2mm
Surface coating: Some high-end products apply an additional UV-curable varnish or PMMA wear-resistant layer over the printing layer, cured by UV lamp irradiation (wavelength 365nm, energy ≥800mJ/cm²), significantly improving surface hardness and wear resistance
Embossing (synchronized texture): Embossing rollers press textures synchronized with the printed pattern (wood grain conduits, stone texture, etc.) onto the edge banding surface, making touch and visual effects consistent
Step 4: Slitting and Winding
Wide edge banding is slit to required width (10-100mm) by longitudinal slitting machine
After slitting, inspected by online thickness gauge and colorimeter
Qualified products are wound into rolls by winder, usually 100-500 meters per roll
Each roll of edge banding must be marked on the end face: production batch number, width, thickness, color number, length
4.2 Melamine Edge Banding Production Process
Step 1: Base Paper Selection
Select high-quality decorative base paper of 70-120g/m², requiring water absorption, wet strength, and opacity to meet standards
Step 2: Impregnation and Drying
Base paper is impregnated with melamine resin (solid content 45-55%) through impregnation tank
Resin impregnation amount controlled by metering rollers (130-180%, based on dry base paper weight)
Dried through vertical or horizontal drying oven (zone temperature 80-160°C), removing volatiles, resin partially pre-cured
Step 3: Cutting and Packaging
Impregnated and dried base paper is slit to required width and wound
Melamine edge banding has high storage environment requirements (temperature 20-25°C, relative humidity 50-60%), preventing moisture absorption and adhesion or premature curing
V. Matching Principles of Edge Banding and Panels
5.1 Thickness Matching
Edge banding thickness selection needs to consider panel type and application scenario:
| Panel Type | Recommended Edge Banding Thickness | Reason |
|---|---|---|
| Thin panels (≤12mm) | 0.4-0.8mm | Too thick edge banding makes edge proportion unbalanced and unattractive |
| Conventional panel furniture (15-25mm) | 0.8-1.5mm | Balances economy and durability, mainstream choice |
| Thick furniture/countertops (≥30mm) | 1.5-3.0mm | Ensures edge impact resistance and machining allowance (chamfering, rounding) |
5.2 Color Matching
Precise color matching is the most critical part of edge banding selection:
Same-color matching: Edge banding and panel surface colors remain consistent, achieving "seamless" visual effect. Recommend using same brand, same batch of facing paper and edge banding to minimize color difference
Contrast matching: Dark panels with light edge banding, or light panels with dark edge banding, forming a contour line effect, commonly used in modern minimalist style
Color Difference Control Technical Means:
Spectrophotometer measures ΔE value, ΔE≤0.5 is invisible to naked eye
Must compare colors in standard light source box (D65 light source, color temperature 6500K)
Consider metamerism phenomenon: ensure edge banding and faced panel have no obvious color difference under all light sources (daylight, warm light, cool white light)
5.3 Adhesive Matching
Different edge banding materials require different hot-melt adhesives and application parameters:
| Edge Banding Material | Recommended Adhesive | Hot-Melt Application Temperature | Edge Banding Machine Speed |
|---|---|---|---|
| PVC (thickness ≤1mm) | EVA hot-melt (high VA content) | 180-210°C | 15-25m/min |
| PVC (thickness >1mm) | PUR hot-melt (moisture-curing) | 130-150°C | 10-18m/min |
| ABS | PUR hot-melt (preferred) | 130-150°C | 12-20m/min |
| Melamine | EVA hot-melt (low temperature) | 160-190°C | 18-28m/min |
| Wood veneer | EVA hot-melt or white glue | 160-200°C | 10-15m/min |
Selection Logic of EVA Hot-Melt vs PUR Hot-Melt:
EVA hot-melt: Economical, long open time, reversible bonding (can re-melt when heated), suitable for conventional PVC edge banding and general furniture applications. Disadvantage: heat and water resistance inferior to PUR.
PUR hot-melt (polyurethane hot-melt): Irreversible bonding, excellent heat, water, and solvent resistance, higher bonding strength, good elasticity. Suitable for ABS edge banding, thick PVC edge banding, kitchen and bathroom furniture (high humidity environment), and export products (long-distance sea transport with high temperature and humidity). Price is about 2-3 times that of EVA.
VI. Common Quality Problems of Edge Banding
6.1 Debonding / Edge Banding Falling Off
Phenomenon: Edge banding separates from panel edge, local or entire strip lifting.
Causes:
Hot-melt adhesive temperature not up to standard (too low: poor wetting; too high: adhesive aging and deterioration)
Insufficient edge banding machine pressure or worn pressure rollers, adhesive layer not fully pressed
Dust, oil, or excessive moisture content (>12%) on panel edge
Hot-melt adhesive open time not matching edge banding machine speed — too fast, adhesive solidifies before pressing
Solutions:
Calibrate edge banding machine glue pot temperature with infrared thermometer
Regularly check pressure roller pressure and flatness to ensure uniform pressing
Blow panel edges with compressed air before edge banding to remove dust
Select hot-melt adhesive model matching edge banding speed (open time 5-15 seconds adjustable)
6.2 Edge Banding Shrinkage / Whitening Exposure
Phenomenon: After edge banding for some time (hours to days), edge banding shrinks in length direction, causing substrate exposure at both ends of panel edge ("whitening exposure").
Causes:
Edge banding has residual stress during production (over-stretched during stretch forming without sufficient annealing)
Edge banding linear expansion coefficient differs greatly from panel, shrinkage not synchronized during temperature changes
Edge banding in winter low-temperature environment, temperature difference aggravates shrinkage
Solutions:
Select high-quality edge banding with sufficient stress release (annealed or online cooling shaped during production)
Store panel and edge banding at same ambient temperature for more than 24 hours before edge banding
Appropriately reduce edge banding machine speed and increase pressing temperature during winter construction
6.3 Glue Overflow / Obvious Glue Line
Phenomenon: Obvious adhesive squeeze-out line visible at the junction of edge banding and panel surface, affecting appearance and difficult to remove.
Causes:
Excessive hot-melt adhesive application amount (conventional amount 150-250g/m², too high causes glue squeeze-out)
Poor panel edge flatness, uneven adhesive distribution
Edge banding machine milling cutter or trimming knife not adjusted properly, overflow glue not synchronously removed
Solutions:
Precisely control glue roller application amount (achieved by adjusting gap or scraper)
Ensure panel edge is straight without waves before edge banding (recommend double-end milling for pre-precision milling)
Select edge banding machine with pre-milling function, mill and trim panel edge before applying glue
6.4 Trimming Whitening (Specific to PVC Edge Banding)
Phenomenon: After PVC edge banding is cut by trimming knife, white marks appear on the cut edge.
Causes:
PVC material undergoes silver streak phenomenon when subjected to shear stress — stress concentration areas form tiny voids and silver streak bands, scattering light and appearing white
Trimming knife not sharp enough, or excessive trimming amount, causing excessive mechanical stress
Excessive filler content (inferior PVC edge banding) aggravates stress whitening
Solutions:
Use trimming knife + scraper combination (rough trim first then fine scrape, reducing residual stress)
Switch to ABS edge banding to fundamentally avoid this problem
Select high-quality PVC edge banding with low filler content and moderate plasticizer content
After trimming, use hot air gun (temperature about 120°C) to slightly heat the cut edge, which can lighten or even restore the white
6.5 Edge Banding Surface Scratches / Loss of Gloss
Phenomenon: Obvious scratches or local gloss decrease on edge banding surface.
Causes:
Impurities or hard particles on edge banding machine pressure roller surface
Tool scraping edge banding surface during trimming
Hard object scratching during subsequent processes (handling, packing)
Solutions:
Regularly clean all moving parts of edge banding machine, keep pressure roller surface clean
Regularly replace trimming blades (recommend replacing every 500-800 meters)
Wrap finished furniture corners with PE protective film before packing to avoid subsequent damage
VII. Technical Development Trends of Edge Banding
7.1 Same-Color Integration and High Simulation
As digital printing technology develops toward industrial-grade applications, edge banding surface effects are evolving toward ultimate simulation:
Synchronized grain matching technology: Edge banding wood grain texture and panel surface texture are continuous and misalignment-free at the joint, achieving "integrated molding" visual effect
3D tactile embossing: Through precise temperature control and embossing processes, reproduce wood conduit depth and tactile feel on edge banding surface
Digital custom printing: Small-batch custom edge banding becomes possible (traditional gravure printing requires plate making, high minimum order quantity), providing more possibilities for personalized furniture design
7.2 Environmental Protection and Lead-Free
Comprehensive popularization of lead-free stabilizers: Calcium-zinc composite stabilizers have basically replaced traditional lead salt stabilizers, ensuring lead content in edge banding is far below RoHS limit requirements
Water-based ink application: Edge banding printing processes gradually use water-based ink to replace solvent-based ink, significantly reducing VOCs emissions
Bio-based plasticizers: Bio-based plasticizers represented by epoxidized soybean oil (ESO) are beginning to be applied in high-end PVC edge banding, further reducing dependence on petrochemical-based raw materials
7.3 Functionalization and Intelligence
Antibacterial edge banding: Add silver ions or nano-zinc oxide antibacterial agents to edge banding surface, inhibiting surface bacterial growth, suitable for hospitals, schools, kitchen furniture
Fragrance-releasing/odor-purifying edge banding: Add low-VOCs slow-release fragrance or formaldehyde-removing factors, continuously releasing light fragrance or decomposing formaldehyde in the air
Sensing edge banding: Embed conductive circuits or RFID tags in the inner layer of edge banding, giving furniture "sensing" or "traceability" functions, suitable for smart furniture and anti-counterfeiting traceability
7.4 Ultra-Thin and Lightweight
To match the minimalist design trend, demand for 0.2-0.3mm ultra-thin edge banding is growing. Such products require materials with higher strength, lower shrinkage, and better bending performance, placing more refined control requirements on formulas and processes.
Frequently Asked Questions (FAQ):
Q1: What is edge banding? What role does it play in panel furniture?
A1:
Edge banding (Edge Banding / Edge Tape) is a narrow strip of decorative and protective material applied to the cut edges of engineered wood panels such as plywood, particleboard, and MDF. It is bonded to the panel edge with adhesive (hot melt or solvent-based glue) to seal and protect the internal structure and improve appearance.
Its core functions can be summarized in four levels:
| Functional Level | Specific Role |
|---|---|
| Physical protection | Seals the cut edge of the panel, blocks water, moisture, and dust intrusion, prevents swelling, delamination, powdering, or mold of the substrate |
| Environmental sealing | Encloses free formaldehyde and VOCs inside the substrate, preventing emission into indoor air |
| Structural reinforcement | Through strong bonding between edge banding and panel edge, enhances impact resistance and wear resistance of the edge |
| Decorative enhancement | Covers the internal layered structure or particle form, giving furniture a unified, refined, and premium appearance |
An old industry saying:
“To judge the quality of a piece of furniture, look first at its edge banding.” The quality of edge banding often directly reflects the technical level of a furniture manufacturer.
Key conclusion:
Although edge banding accounts for only a very small proportion of material cost (usually less than 3–5%), it has a decisive impact on product service life, environmental performance, appearance quality, and safety.
Q2: What are the main types of edge banding? What are the differences between PVC, ABS, melamine, wood veneer, and metal edge banding?
A2:
The mainstream edge banding products on the market can be divided into five categories:
| Type | Material Composition | Thickness Range | Characteristics | Applications |
|---|---|---|---|---|
| PVC edge banding | PVC resin + calcium carbonate + plasticizer + stabilizer + colorant | 0.4–3.0 mm | Economical, flexible, rich colors, most mainstream | Panel furniture, cabinets, office furniture |
| ABS edge banding | Acrylonitrile-butadiene-styrene copolymer | 0.8–2.0 mm | Pure material, no whitening after trimming, premium feel, better weather resistance than PVC | High-end furniture, kitchen and bath, children's furniture, export products |
| Melamine edge banding | Melamine impregnated paper | 0.2–0.8 mm | High color matching, good adhesion, stable dimensions, but relatively brittle | Matching edge banding for melamine panels |
| Wood veneer edge banding | Natural wood veneer (oak, walnut, cherry, etc.) | 0.3–0.6 mm | Natural and realistic texture, excellent feel, blends with solid wood veneer furniture | High-end solid wood furniture, natural veneer furniture |
| Metal edge banding (aluminum alloy) | Aluminum alloy profile | 1.0–3.0 mm | Sturdy and durable, excellent fire and moisture resistance, modern feel | Commercial furniture, laboratory furniture, office partitions, kitchen countertops |
Key conclusion:
PVC offers the best cost-performance and widest application; ABS offers better overall performance for high-end markets; melamine is suitable for same-color matching; wood veneer provides natural texture; metal edge banding is suitable for special commercial scenarios.
Q3: What is the difference between PVC and ABS edge banding? How to choose?
A3:
PVC edge banding accounts for about 70% of the global edge banding market, while ABS edge banding is rapidly rising in the high-end market. The core differences are:
| Comparison Dimension | PVC Edge Banding | ABS Edge Banding |
|---|---|---|
| Trimming effect | Cut edge tends to whiten (stress whitening) | No whitening after trimming, edge retains material color |
| Weather resistance | Glass transition temperature about 80 °C | Glass transition temperature about 105 °C, more stable at high temperatures, less brittle at low temperatures |
| Material purity | Contains calcium carbonate filler (15–25%) | Contains no filler or very little special filler, more uniform material |
| Environmental performance | Contains plasticizers, phthalates must be controlled | Non-toxic, odorless, low smoke when burned, no hydrogen chloride corrosive gas |
| Price | Economical | About 1.5–2.5 times that of PVC |
| Applications | General panel furniture, cabinets, office furniture | High-end furniture, kitchen and bath, children's furniture, export products |
Selection advice:
Limited budget, standard furniture: choose PVC edge banding.
High-end furniture, export products, humid kitchen and bath environments: choose ABS edge banding.
Pursuing clean trimming and sharp edge lines: ABS is the first choice.
Key conclusion:
ABS edge banding does not whiten when trimmed, has better weather resistance and environmental performance, but is more expensive; PVC is economical, flexible, and color-rich. Choose according to product positioning and budget.
Q4: How to choose the thickness of edge banding? What thickness corresponds to different panels?
A4:
Edge banding thickness selection depends on panel type and application:
| Panel Type | Recommended Edge Banding Thickness | Reason |
|---|---|---|
| Thin panels (≤12 mm) | 0.4–0.8 mm | Too thick edge banding distorts edge proportions and looks unattractive |
| Standard panel furniture (15–25 mm) | 0.8–1.5 mm | Balances economy and durability, mainstream choice |
| Thick furniture/countertops (≥30 mm) | 1.5–3.0 mm | Ensures edge impact resistance and processing allowance (chamfering, rounding) |
Key conclusion:
Thin panels use thin edge banding, standard furniture uses 0.8–1.5 mm, thick panels or countertops use 1.5–3.0 mm. Thickness selection should consider appearance, durability, and processing needs.
Q5: How environmentally friendly is edge banding? Does it contain formaldehyde? How to judge whether it is environmentally friendly?
A5:
The environmental performance of edge banding mainly depends on the material and adhesive:
| Type | Environmental Performance | Explanation |
|---|---|---|
| PVC edge banding | Heavy metals and phthalates must be controlled | High-quality products use calcium-zinc stabilizers and DOTP/TOTM eco-friendly plasticizers, compliant with RoHS and REACH |
| ABS edge banding | Better environmental performance | Non-toxic, odorless, low smoke when burned, no hydrogen chloride corrosive gas |
| Melamine edge banding | Relatively good environmental performance | Based on melamine impregnated paper, no harmful substances |
| Wood veneer edge banding | Natural and environmentally friendly | Natural wood veneer, no chemical additives |
| Metal edge banding | Environmentally friendly | Aluminum alloy, recyclable |
Key testing indicators:
Heavy metal content (RoHS Directive): lead, mercury, cadmium, hexavalent chromium below limits.
Phthalate content: total non-phthalate plasticizers ≤1000 mg/kg.
VOC emission: TVOC ≤100 μg/m³ (ISO 16000-6).
Key conclusion:
High-quality edge banding should comply with RoHS and REACH, with no irritating odor. When purchasing, look for test reports and environmental labels. ABS has the best environmental performance; PVC requires eco-friendly plasticizers.
Q6: What are the common quality problems of edge banding? How to solve them?
A6:
Common quality problems and solutions:
| Problem | Phenomenon | Main Causes | Solutions |
|---|---|---|---|
| Glue failure/edge banding falling off | Edge banding separates from panel edge | Incorrect hot melt temperature, insufficient pressure, dust or high moisture on panel edge, open time not matching speed | Calibrate glue pot temperature, check pressure rollers, clean panel edge, select matching hot melt adhesive |
| Edge banding shrinkage/whitening | After hours to days, edge banding shrinks in length, exposing substrate at panel ends | Residual stress in edge banding, different linear expansion coefficient, low-temperature application in winter | Use high-quality stress-relieved edge banding, store panel and edge banding at same temperature for 24 hours, reduce speed and increase temperature in winter |
| Glue overflow/visible glue line | Visible glue line at the junction of edge banding and panel surface | Excessive glue amount, poor panel edge flatness, trimming knife not adjusted | Precisely control glue amount, pre-mill panel edge, use edge banding machine with pre-milling function |
| Trimming whitening (PVC-specific) | White marks on cut edge after trimming PVC edge banding | Stress whitening, dull trimming knife, high filler content | Use trimming knife + scraper combination, switch to ABS edge banding, choose high-quality PVC edge banding, slightly heat cut edge with heat gun |
| Surface scratches/loss of gloss | Scratches or localized gloss loss on edge banding surface | Impurities on pressure rollers, trimming knife scraping, scratches during handling | Regularly clean edge banding machine, replace trimming blades regularly, wrap corners with PE protective film before packaging |
Key conclusion:
Quality problems are mostly related to process parameters, equipment condition, and material matching. They can be effectively solved by precise temperature control, optimized glue amount, and regular equipment maintenance.
Q7: How to match edge banding with panels? How to choose thickness, color, and adhesive?
A7:
Matching edge banding with panels involves three dimensions:
1. Thickness matching:
| Panel Type | Recommended Edge Banding Thickness |
|---|---|
| Thin panels (≤12 mm) | 0.4–0.8 mm |
| Standard panel furniture (15–25 mm) | 0.8–1.5 mm |
| Thick furniture/countertops (≥30 mm) | 1.5–3.0 mm |
2. Color matching:
Same-color matching: edge banding color consistent with panel surface for “seamless” effect. Same brand and batch recommended.
Contrast matching: dark panel with light edge banding or vice versa, creating contour line effect, common in modern minimalist style.
Color difference control: ΔE measured by spectrophotometer, ΔE≤0.5 is invisible to the naked eye; compare in standard light booth (D65); consider metamerism.
3. Adhesive matching:
| Edge Banding Material | Recommended Adhesive | Hot Melt Temperature | Edge Banding Machine Speed |
|---|---|---|---|
| PVC (≤1 mm) | EVA hot melt (high VA content) | 180–210 °C | 15–25 m/min |
| PVC (>1 mm) | PUR hot melt (moisture-curing) | 130–150 °C | 10–18 m/min |
| ABS | PUR hot melt (first choice) | 130–150 °C | 12–20 m/min |
| Melamine | EVA hot melt (low temperature) | 160–190 °C | 18–28 m/min |
| Wood veneer | EVA hot melt or white glue | 160–200 °C | 10–15 m/min |
EVA vs. PUR:
EVA: economical, long open time, reversible bonding, suitable for standard PVC edge banding and general furniture.
PUR: irreversible bonding, excellent heat, water, and solvent resistance, higher bonding strength. Suitable for ABS, thick PVC, kitchen and bath furniture, and export products. Price about 2–3 times that of EVA.
Key conclusion:
Thickness according to panel, color preferably same-color matching, adhesive according to edge banding material and application. EVA for standard, PUR for high-end and humid environments.
Q8: What is the production process of edge banding? How are PVC and ABS edge banding produced?
A8:
Edge banding production is mainly divided into PVC/ABS edge banding and melamine edge banding.
PVC/ABS edge banding production process:
Step 1: Mixing
PVC resin, plasticizer, stabilizer, filler, colorant, UV additives weighed according to formula.
Mixed in high-speed mixer (80–120 °C), cooled and transferred to storage hopper.
Step 2: Extrusion
Mixture plasticized in single or twin-screw extruder (barrel temperature 160–200 °C).
Melt extruded through T-die into thin sheet.
Sheet calendered by three-roll calender (120–150 °C) for precise thickness and smooth surface.
Step 3: Surface treatment (printing and texture)
Printing layer: gravure or flexographic printing, registration accuracy ≤0.2 mm.
Surface coating: UV-curable varnish or PMMA wear layer, UV lamp curing.
Embossing: embossing roller presses synchronized texture with printed pattern.
Step 4: Slitting and winding
Slitting machine cuts to required width (10–100 mm).
Inline thickness and color difference inspection.
Winding machine rolls into coils, 100–500 m per roll.
End face marked with production batch, width, thickness, color code, length.
Melamine edge banding production process:
Base paper selection: 70–120 g/m² high-quality decorative base paper.
Impregnation and drying: impregnated with melamine resin (solid content 45–55%), metering roller controls impregnation amount (130–180%), drying oven (80–160 °C).
Cutting and packaging: slit to required width, storage environment 20–25 °C, relative humidity 50–60%.
Key conclusion:
PVC/ABS edge banding is produced by mixing, extrusion, calendering, printing, embossing, and slitting; melamine edge banding by base paper impregnation, drying, and cutting. Process control directly affects quality.
Q9: What are the technology development trends of edge banding?
A9:
Edge banding technology is developing toward color integration, environmental friendliness, functionality, and ultra-thinness:
1. Color integration and high simulation:
Synchronized pattern matching: edge banding wood grain and panel surface texture continuous at the joint, achieving “one-piece” visual effect.
3D tactile embossing: precise temperature control and embossing process reproduce wood pore depth and touch.
Digital custom printing: small-batch custom edge banding becomes possible, providing more possibilities for personalized furniture design.
2. Environmental friendliness and lead-free:
Lead-free stabilizers fully popularized: calcium-zinc composite stabilizers replace lead salt stabilizers, lead content far below RoHS limits.
Water-based ink application: replaces solvent-based ink, greatly reducing VOC emissions.
Bio-based plasticizers: epoxidized soybean oil (ESO) and other bio-based plasticizers begin to be applied, reducing dependence on petrochemical raw materials.
3. Functionality and intelligence:
Antibacterial edge banding: silver ions or nano-zinc oxide antibacterial agents added, inhibiting bacterial growth, suitable for hospitals, schools, kitchen furniture.
Fragrance/odor-purifying edge banding: slow-release fragrance or formaldehyde-decomposing factors added, continuously releasing light fragrance or decomposing formaldehyde.
Sensor edge banding: conductive circuits or RFID tags embedded, giving furniture “sensing” or “traceability” functions, suitable for smart furniture and anti-counterfeiting.
4. Ultra-thin and lightweight:
Demand for 0.2–0.3 mm ultra-thin edge banding is growing, requiring higher strength, lower shrinkage, and better bending performance.
Key conclusion:
Edge banding is developing from single-function material to high-simulation, environmentally friendly, functional, and intelligent products, better meeting personalized furniture and smart home needs.
Q10: How to judge the quality of edge banding? What are the key indicators?
A10:
Judging edge banding quality requires attention to the following key indicators:
| Indicator | Test Method | High-Quality Standard | Poor Performance |
|---|---|---|---|
| Flexibility (cold bending) | 180° bending at -5 °C | No cracks | Breakage or whitening |
| Heat resistance | 200 °C hot press test | Does not stick to panel, does not discolor | Melts and sticks, severe discoloration |
| Wear resistance (Taber) | CS-17 wheel, 500 g load | Pattern clear after 500 cycles | Pattern disappears or worn through |
| Color difference (ΔE) | Colorimeter between batches | ΔE≤0.5 (invisible) | ΔE≥1.0 (visible) |
| Gloss deviation | Multi-point measurement in same batch | ≤±3 GU | ≥±8 GU |
| Peel strength | 180° peel test | ≥1.5 N/mm (qualified), ≥2.5 N/mm (high quality) | Low, easy to debond |
| Thermal cycling resistance | 63 °C / -20 °C for 2 h each, 5 cycles | No cracking, debonding, or discoloration | Cracking, debonding, discoloration |
| Aging resistance (xenon) | 500 h exposure | ΔE≤2.0, peel strength retention ≥80% | Large color difference, significant strength loss |
| Environmental performance | Heavy metals, phthalates, VOCs | Compliant with RoHS, REACH; TVOC≤100 μg/m³ | Exceeds limits, irritating odor |
Appearance requirements:
Smooth and uniform surface, no bubbles, particles, pits, or scratches.
Consistent color: same batch ΔE≤0.5, different batches ΔE≤1.0.
Straight edges for continuous feeding in automatic edge banding machines.
Clear printing: accurate registration (≤0.2 mm), no ghosting.
Dimensional accuracy (LY/T 2383-2014):
Width: ±0.15 mm (≤50 mm), ±0.20 mm (>50 mm).
Thickness: ±0.03 mm (≤1.0 mm), ±0.05 mm (>1.0 mm).
Length: ±3 mm/100 m.
Key conclusion:
Judging edge banding quality requires comprehensive consideration of appearance, dimensional accuracy, physical and mechanical properties, and environmental safety. High-quality edge banding is flexible, heat and wear resistant, has small color difference, high peel strength, and meets environmental standards.
JINDIWOOD · Engineered for Certainty — From every micron of dimensional accuracy in edge banding to every bonding peel strength, we protect every detail of your furniture with certain quality standards.
This article is an original technical article by JINDIWOOD. Reproduction must indicate the source.