中文
 繁體中文
 日本語
 English
 Deutsch
 Español
 Français
 العربية
 Italiano
 한국어
 Nederlands
 Português
 Русский
 Türkçe
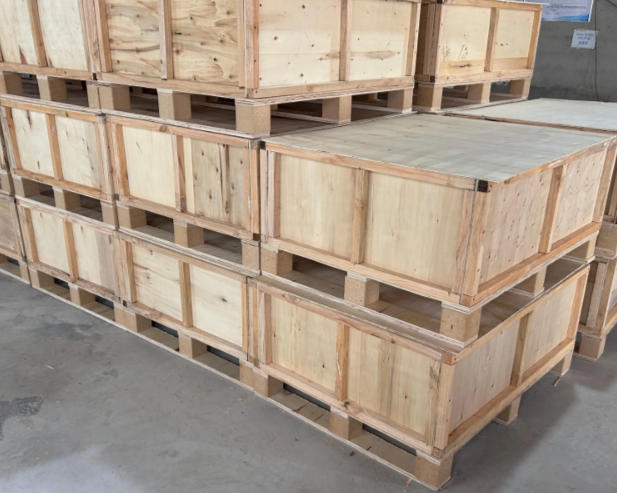
I. Basic Concept of Packing Plywood
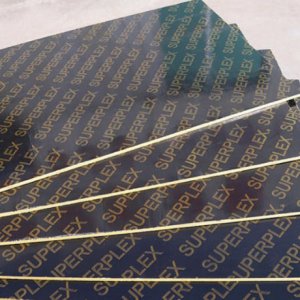
Packing plywood (also known as container plywood, industrial packaging board) is a specialized plywood engineered specifically for industrial product transportation packaging, warehousing logistics, and export containerization. It is manufactured by rotary-peeling logs into veneers, bonding them with adhesives, and hot-pressing into panels. It features high strength, impact resistance, moisture and decay resistance, and is exempt from fumigation. It serves as the core material for manufacturing transport crates, wooden pallets, dunnage, separators, and other industrial logistics appliances.
In modern logistics systems, packing plywood plays the role of an "invisible armor" — it wraps around heavy machinery, precision instruments, electronic products, and fresh produce, withstanding stacking, forklift operations, long-haul vibrations, and temperature-humidity fluctuations, ensuring goods arrive intact from factory to end-user.
Industry Status & Market Size:
According to the China Packaging Federation, the market size of wooden packaging products in China exceeded RMB 120 billion in 2025, of which plywood-based packaging materials accounted for approximately 35% (about RMB 42 billion). With the increasing complexity of global supply chains and the explosive growth of cross-border e-commerce (China's cross-border e-commerce import/export volume exceeded RMB 2.5 trillion in 2025), the demand for packing plywood continues to rise. Global annual consumption of plywood for packaging exceeded 8 million cubic meters in 2025, with China being the largest producer and exporter, accounting for over 60% of global output.
Core Advantages – Why Packing Plywood Replaces Solid Wood Packaging:
Fumigation-Free (Key Advantage): The high-temperature hot-pressing process during plywood manufacturing (>140°C, lasting several minutes to tens of minutes) is sufficient to kill eggs, larvae, and adult insects in the wood. The heat-treated (HT) plywood can be directly used for export packaging without additional fumigation (ISPM 15), simplifying export procedures and reducing costs.
High Strength & Impact Resistance: The cross-laminated multi-layer veneer structure provides uniform mechanical properties, with bending strength and impact resistance superior to solid sawn timber of the same thickness (especially solid wood with knots, which may fracture at knots under impact loads).
Cost Advantage: High raw material utilization (80-85%), using small-diameter logs and fast-growing species (poplar, pine, eucalyptus), resulting in costs 30-50% lower than solid wood packaging of the same specifications.
Standardized Dimensions: Enables mass production of standard sizes (1220×2440mm and various custom sizes), facilitating automated packaging lines (e.g., automatic nailing machines, strapping machines).
Excellent Workability: Easy to saw, nail, groove, drill, and mill, with good compatibility with various connectors (nails, screws, L-brackets, strapping).
II. Classification System of Packing Plywood
2.1 By Water Resistance Grade (GB/T 24311-2021 Plywood for Combined Packaging Boxes)
This is the most critical classification dimension, directly affecting application scenarios and bonding strength requirements:
| Water Resistance Grade | Code | Adhesive Type | Suitable Environment | Bonding Strength Requirement (MPa) | Typical Applications |
|---|---|---|---|---|---|
| Class I (High Water Resistance) | WBP (Water Boil Proof) | Phenolic resin (PF) or melamine-modified phenolic | Humid/outdoor environment, long-term high humidity or short-term water immersion (e.g., condensation in sea containers, outdoor rain) | ≥0.70 (with wood failure ≥60%) | Export sea freight (container shipping, long voyage, high humidity), tropical storage, refrigerated packaging |
| Class II (Moisture Resistant) | MR (Moisture Resistant) | Melamine-modified urea-formaldehyde (MUF) | General storage and transport (dry to medium humidity, no long-term immersion risk) | ≥0.60 | Conventional inland transport, standard warehouse shelving, e-commerce logistics |
| Class III (Non-water-resistant / Dry state) | Standard | Urea-formaldehyde (UF) | Dry environment (indoor storage, short turnover, no significant humidity fluctuations) | ≥0.50 | Single-use packaging, low-value goods packaging, express filler dividers |
Selection Logic for Water Resistance Grade:
Export sea freight (especially long-haul routes >15 days): Must choose Class I (WBP grade), as temperature differences inside shipping containers can exceed 20°C, generating significant condensation ("container rain"), exposing packaging to prolonged high humidity. Standard UF-bonded panels may delaminate within 3-5 days.
Inland transport (truck/rail, 2-5 days): Class II (MR grade) suffices.
Indoor short-term turnover (<3 days): Class III meets basic needs.
JINDIWOOD Export-Grade Packing Plywood:
Uses phenolic resin adhesive (WBP grade), withstands boiling water for 4 hours without delamination (tested per GB/T 17657), fully meeting the high-humidity requirements of sea containers.
Supplied with ISPM 15 Heat Treatment (HT) mark and fumigation certificates (upon request) to ensure smooth customs clearance.
Available faces: bleached poplar (clean appearance), mahogany/okoume (premium appearance for high-value goods), or plain unfinished (economical).
2.2 By Face Veneer Type
| Face Type | Appearance Features | Strength & Durability | Applications |
|---|---|---|---|
| Bleached Poplar | White, clean, flat surface, minimal or no knots | Moderate (medium strength and wear resistance), but highest appearance grade | Export packaging for high-value products (electronics, precision instruments, medical devices) — enhances brand image |
| Mahogany/Okoume | Attractive grain, warm color (reddish-brown), higher density | Good (higher surface hardness and impact resistance) | High-end consumer goods, furniture, artwork packaging |
| Mixed Hardwood | Darker color (brown to dark brown), some knots, coarse grain | Moderate (balanced strength, cost-effective) | General industrial products, machinery, tool packaging |
| Pine | Light yellow, straight grain, higher resin content | Higher (resin imparts some water resistance and strength) | Heavy industrial products, construction machinery, automotive parts packaging |
| Raw (Unfaced) | Retains core color (light yellow to light brown), visible veneer joints | Standard (strength of core species) | Economical packaging, single-use crates, pallets |
2.3 By Core Species
| Core Type | Species Mix | Density (g/cm³) | Characteristics | Cost | Applications |
|---|---|---|---|---|---|
| Poplar Core | 100% Poplar | 0.40-0.50 | Light, soft, light color, easy to machine, good cushioning | Low | Light product packaging, electronics, daily goods |
| Pine Core | 100% Pine | 0.45-0.55 | Higher strength, natural resin (slightly better water resistance), attractive grain | Medium | General industrial goods, mechanical parts, building materials |
| Eucalyptus Core | 100% Eucalyptus | 0.55-0.65 | High density, high strength, hardness, smooth surface | Medium-High | Heavy machinery, automotive parts, precision instruments |
| Mixed Hardwood Core | Poplar+Eucalyptus+mixed | 0.45-0.60 | Balanced properties (leverages advantages of various woods for cost-performance) | Medium | General-purpose packaging, most widely used |
| Birch Core | 100% Birch | 0.60-0.70 | Dense, extremely high strength, fine surface, excellent impact resistance | High | Premium products, export-grade heavy goods, military packaging |
Economic Selection Principles:
Low strength requirement (load <100kg) → Poplar core (lowest cost, sufficient)
Moderate strength requirement (100-500kg) → Mixed hardwood (best cost-performance, mainstream)
High strength requirement (>500kg) or humid environment → Eucalyptus/Pine core (strength and moisture resistance)
Extremely high requirements for both strength and appearance → Birch core (high cost, only for special needs)
2.4 By Thickness
| Thickness Range | Common Thickness (mm) | Typical Applications |
|---|---|---|
| Thin (3-5mm) | 3, 4, 5 | Liners for small products, thin packaging boxes, photo frame backs, craft bases |
| Medium (6-12mm) | 6, 7, 8, 9, 10, 12 | Standard crates (general industrial goods, daily necessities, electronics), shelf dividers, pallet decks |
| Thick (15-25mm) | 15, 18, 20, 22, 25 | Heavy machinery crates (construction machinery, automotive parts, industrial equipment), overall frames for large equipment, heavy-duty pallets |
| Extra Thick (≥30mm) | 30, 35, 40, 50 (custom) | Ultra-heavy/oversized equipment packaging (generator sets, large machine tools, wind power equipment), foundation support structures, load-bearing bases |
Thickness Selection Reference (Based on packaging design empirical values):
| Package Weight | Recommended Box Thickness | Recommended Pallet Deck Thickness | Recommended Divider Thickness |
|---|---|---|---|
| <50 kg | 6-9 mm | 12-15 mm | 3-5 mm |
| 50-200 kg | 9-12 mm | 15-18 mm | 5-8 mm |
| 200-500 kg | 12-15 mm | 18-22 mm | 8-10 mm |
| 500-1000 kg | 15-18 mm | 22-25 mm | 10-12 mm |
| >1000 kg | 18-25 mm (or thicker) | ≥25 mm | ≥12 mm |
III. Manufacturing Raw Materials & Adhesives for Packing Plywood
3.1 Wood Raw Materials
Packing plywood has lower veneer grade requirements compared to furniture-grade and construction-grade plywood, consistent with its positioning as an "industrial function" rather than "aesthetic function" material:
| Raw Material Requirement | Packing Grade Standard | Furniture Grade Comparison (Reference) |
|---|---|---|
| Veneer Grade | Allows minor knots (live knots ≤30mm, dead knots must be repaired), cracks (≤5mm wide), color variation | No knots (premium grade), no cracks, no color variation |
| Core Splicing | Splicing allowed (longitudinal extension, lateral widening), gaps ≤3mm | Splicing gaps ≤1mm |
| Face Grade | Allows minor repairs and color variation (e.g., a thin bleach layer on the surface is acceptable) | Premium grade: no repairs on surface, uniform color |
| Moisture Content | 6-14% (national standard) | 6-12% (more stringent) |
3.2 Adhesive Systems — Determining the Water Resistance Grade of Packing Plywood
| Adhesive Type | Water Resistance Grade | Characteristics | Cost | Applications |
|---|---|---|---|---|
| Urea-Formaldehyde (UF) | Class III (Dry) | Fast curing, acceptable bonding strength, lowest cost, but not water-resistant | Very Low | Dry environment single-use packaging, low-value products |
| Melamine-Modified Urea-Formaldehyde (MUF) | Class II (Moisture Resistant) | Better water resistance than UF, moderate cost | Medium | General warehousing and transport, inland logistics |
| Phenolic Resin (PF / WBP Grade) | Class I (High water resistance, boil-proof) | Withstands boiling water, excellent weather resistance, dark color (reddish-brown glue line), higher cost | High | Export sea freight, humid environments, high-value products |
| Mixed Adhesive (UF+PF blend) | Between Class II and Class I | Balances cost and performance, bonding strength slightly lower than pure PF | Medium-High | Scenarios with some water resistance requirements but limited budget |
JINDIWOOD Export-Grade Packing Plywood Adhesive Strategy:
Standard products: MUF adhesive, Class II (moisture resistant), meeting general export and domestic needs.
Sea freight/high-humidity environments: PF adhesive (WBP grade), Class I, capable of withstanding container humidity and short-term immersion.
Environmental grades: All reach E1 (≤0.050mg/m³), with custom products available up to E0 (≤0.025mg/m³).
IV. Manufacturing Process Characteristics of Packing Plywood
The production process for packing plywood is generally consistent with standard plywood (see Complete Analysis of Plywood Production). However, due to packaging applications' requirements for cost control and mass standardized production, the following stages have significantly different characteristics:
4.1 Veneer Grading & Lay-up Optimization
Relaxed Grading: Packing-grade plywood does not require A/B grade veneers (furniture grade). It allows extensive use of C/D grade veneers (with repair marks, slight discoloration, minor knots), significantly reducing raw material costs (30-50% lower than furniture-grade veneers).
Simplified Lay-up (Cross-structure maintained): Still follows the principle of "adjacent veneers with perpendicular fiber directions, odd-number of layers." However, core veneer splicing requirements are relaxed (gaps ≤3mm, overlap area ≤5%), improving production efficiency.
4.2 Adhesive Application Control
Glue application amount is lower than furniture-grade plywood (lower bonding strength requirements), typically 150-200g/m² (both sides combined), compared to 200-260g/m² for furniture grade.
Glue roller gaps can be slightly wider (saving adhesive), but must ensure continuous glue lines without breaks.
4.3 Hot Pressing Process (Focus on Efficiency Rather Than Ultimate Performance)
| Parameter | Packing Grade | Furniture Grade |
|---|---|---|
| Hot Pressing Temperature | 120-160°C (depending on adhesive type) | 120-160°C |
| Hot Pressing Pressure | 1.0-1.8 MPa | 1.5-2.5 MPa |
| Press Factor | 0.5-0.8 min/mm | 0.8-1.0 min/mm |
| Output Speed | Higher (large volume, faster cycle) | Lower |
4.4 Sanding Requirements (Lower than Furniture Grade)
Packing boards typically undergo light sanding on one or both sides (sanding belt grit 120-150 mesh), removing surface burrs and minor unevenness. Surface roughness requirement Ra≤6.3μm (furniture grade requires Ra≤3.2μm).
Some low-end packing boards are not sanded at all ("raw" delivery), retaining the natural hot-pressed surface to further reduce costs.
4.5 Packaging & Labeling
Packaging: Standard moisture-proof packaging (plastic film wrapping + edge protectors). Protection requirements are lower than furniture boards (as the end use is also packaging, its own protection level can be one grade lower).
Labeling Requirements: Export-grade packing plywood must bear the ISPM 15 Heat Treatment (HT) mark and production batch number. Some customers require "Made in China" and product grade information.
V. Core Technical Specifications of Packing Plywood
5.1 Physical & Mechanical Performance Requirements (GB/T 24311-2021 Plywood for Combined Packaging Boxes)
| Performance Indicator | Unit | Class I (High Water Resistance) | Class II (Moisture Resistant) | Class III (Dry) | Test Standard |
|---|---|---|---|---|---|
| Bonding Strength (Average) | MPa | ≥0.70 | ≥0.60 | ≥0.50 | GB/T 17657 |
| Minimum Veneer Bonding Strength | MPa | ≥0.60 | ≥0.50 | ≥0.40 | GB/T 17657 |
| Moisture Content | % | 6-14 | 6-14 | 6-14 | GB/T 17657 (Gravimetric) |
| Modulus of Rupture (Parallel, ≥12mm) | MPa | ≥40 | ≥35 | ≥30 | GB/T 17657 (3-point bending) |
| Modulus of Rupture (Perpendicular, ≥12mm) | MPa | ≥25 | ≥20 | ≥18 | GB/T 17657 |
| Modulus of Elasticity (Parallel) | MPa | ≥6000 | ≥5000 | ≥4500 | GB/T 17657 |
| Delamination Resistance | — | Delamination ≤5% (no visible glue line cracking) | Delamination ≤10% | Delamination ≤15% | Immersion test (63±3°C water, 3h + drying) |
| Face Thickness (Single Side) | mm | ≥0.3 | ≥0.3 | ≥0.3 | Caliper measurement |
JINDIWOOD Export-Grade Packing Plywood Internal Standards (Above National Requirements):
Bonding Strength ≥0.9 MPa (Class I), ensuring long-term reliability in sea freight and high-humidity environments.
Moisture Content controlled at 8-11% (mid-range of the strict interval), balancing strength and moisture resistance.
Modulus of Rupture ≥45 MPa (parallel), ensuring no fracture under heavy cargo stacking.
5.2 ISPM 15 Heat Treatment (HT) Standard (Essential for Export)
ISPM 15 (International Standards for Phytosanitary Measures No. 15) is the international standard that all wooden packaging materials must comply with for export. Core requirements:
| Treatment Method | Treatment Parameters | Labeling Requirements | Applicability |
|---|---|---|---|
| Heat Treatment (HT) | Wood core temperature ≥56°C for ≥30 minutes (plywood far exceeds this during hot pressing; its manufacturing process naturally satisfies HT) | IPPC logo branded or sprayed on boards/crates, format: XX-00000-HT | Most countries (including EU, USA, Australia, etc.) |
| Fumigation (MB, Methyl Bromide) | Methyl bromide (CH₃Br) fumigation in enclosed space per ISPM 15 specifications | IPPC logo format: XX-00000-MB | Some countries or special requirements (being phased out due to environmental/health concerns) |
JINDIWOOD Commitment: All export-grade packing plywood is supplied with ISPM 15 HT marks and fumigation/heat treatment certificates (upon request) for customs clearance. Customers may also request phytosanitary certificates for even smoother clearance.
5.3 Impact Resistance & Stacking Performance (Key Parameters for Packaging Design)
Although not mandatory in the national standard, impact resistance (drop weight or ball impact test) and stacking strength (compressive strength) are highly valued by packaging designers:
| Performance Parameter | Typical Value (18mm, Class I) | Significance |
|---|---|---|
| Impact Strength (Izod, unnotched) | 8-12 kJ/m² | Resistance to impact damage from drops or forklift collisions |
| Stacking Compression Strength (short direction) | 15-25 kN/m (across panel width) | Vertical pressure resistance during warehouse stacking (3-5 layers), preventing lower crates from collapsing |
| Nail Holding Power (withdrawal resistance) | 700-1000 N (face), 500-700 N (edge) | Resistance to nail withdrawal, ensuring secure connections without loosening |
VI. Application Scenarios of Packing Plywood
6.1 Industrial Equipment & Machinery Packaging
This is the most important application area for packing plywood:
| Packaging Object | Recommended Product | Recommended Thickness (mm) | Key Requirements |
|---|---|---|---|
| Heavy Machinery (machine tools, excavators, crane parts) | Class I/II (mixed hardwood core) | 18-25 (body) / 25-40 (base) | Ultra-high compression strength (stacking), impact resistance (lifting), waterproof (outdoor storage) |
| Medium Equipment (generators, pumps, compressors) | Class II (mixed hardwood or pine core) | 12-18 (body) / 18-22 (base) | Good bending strength and nail holding power |
| Precision Instruments (medical devices, measuring instruments, electronics) | Class I (bleached poplar or okoume face) | 9-15 | Clean appearance, flat surface, moisture-proof (typically with aluminum foil bags + desiccants inside) |
Typical Case — Heavy Machinery Packaging Solution:
Crate Structure: Heavy-duty wooden base (skids) + surrounding plywood panels (18-25mm) + top rain cover + internal support frame.
Connection Method: L-brackets or galvanized steel straps at corners, M10-M16 bolts at critical nodes, ensuring no deformation during lifting and transport.
6.2 Export Logistics & Container Transport
Export logistics is the second-largest application area and JINDIWOOD's focus:
| Product Type | Recommended Specifications | Key Requirements | JINDIWOOD Advantages |
|---|---|---|---|
| Wooden Crates (export standard) | 1220×2440×(9-18)mm | ISPM 15 HT mark, Class I water resistance (WBP) | Full series Class I water resistance, HT mark included, compliant with customs requirements of all countries |
| Wooden Pallets (Euro/US standard) | Deck 15-22mm, bottom 15-18mm | ISPM 15 HT mark, bending strength ≥40MPa | EPAL certification subcontracting available, meeting EU requirements |
| Dunnage/Divider Panels (container lining) | 6-12mm, custom sizes | Water-resistant, flat, economical | Custom cutting for bulk orders, reducing on-site waste |
6.3 E-Commerce Logistics & Warehousing
With the explosive growth of e-commerce and express delivery, demand for lightweight, standardized packing plywood is strong:
| Application Scenario | Recommended Thickness (mm) | Characteristics | Requirements |
|---|---|---|---|
| E-commerce express crates (replacing corrugated boxes for heavy goods) | 3-6 | Lightweight, low cost, single use | Class III (dry) sufficient, cost priority |
| Warehouse shelf dividers (shelving panels) | 9-15 | Load-bearing (200-500kg/m²), flat | Class II (moisture resistant), anti-corrosion |
| Returnable/reusable packaging crates (cycling use) | 9-18 | Repeated use (20-50 cycles), high strength, impact resistant | Class I (high water resistance) + high-strength core (eucalyptus/mixed hardwood) |
6.4 Special Applications
| Application Scenario | Requirements | Recommended Product | Notes |
|---|---|---|---|
| Cold Chain / Refrigerated Packaging | Low-temperature resistance (-20°C no brittleness) + high moisture protection | Class I (birch or pine core) + surface lamination (moisture-proof aluminum foil or melamine) | Ensure adhesives don't become brittle at low temperatures; wood retains toughness |
| Anti-Static Packaging (Electronic Components) | Surface resistivity ≤10⁹Ω | Packing plywood coated with anti-static paint or film | Prevents static damage to sensitive components |
| Fire-Retardant Packaging (Chemicals / Dangerous Goods) | Fire rating B1 (difficult to ignite) | Class I panels with flame retardant additives | Complies with fire safety regulations for dangerous goods transport packaging |
VII. Quality Identification & Selection of Packing Plywood
7.1 Visual Inspection (Quick Assessment)
| Inspection Item | High-Quality Packing Board Performance | Poor-Quality Packing Board Performance |
|---|---|---|
| Board Surface | Flat, no obvious waves, uniform color (bleached: light white), no oil stains, no mold | Visible warping or depressions, dark color with patches, oil stains or mold spots |
| Board Edge (Cross-section) | Neat cut, visible dense glue lines (darker color), no gaps between veneers, no signs of delamination | Rough cut, thin or intermittent glue lines, visible inter-layer gaps, visible bubbles in glue lines |
| Thickness | Thickness deviation ≤±0.3mm within the same board | Thickness deviation ≥±0.5mm (possible skimping on sanding or hot pressing) |
| Tap Test | Clear, consistent sound (solid structure) | Dull or hollow sound (possible internal delamination or voids) |
7.2 Simple Physical Performance Tests
Water Immersion Test (Quick assessment of water resistance): Cut a 50×50mm sample, immerse in room-temperature water for 24 hours, then observe:
High Quality (Class I/II): No delamination, no significant swelling (thickness increase ≤5%), no glue line cracking.
Poor Quality: Obvious delamination, white lines or cracks in glue lines, thickness increase >10%.
Boiling Water Test (For Class I panels, destructive test): Cut a sample, immerse in boiling water for 4 hours (simulating extreme high humidity), then observe:
High Quality (Class I): No delamination, no blistering, thickness increase ≤8%.
Poor Quality: Delamination, blistering, or thickness increase >15%.
7.3 Selection Guidelines — Match Actual Needs, Avoid Over-Investment
| Application Scenario | Recommended Grade | Recommended Core | Recommended Face | Notes |
|---|---|---|---|---|
| Export Sea Freight (Overseas) | Class I (PF/WBP) | Mixed Hardwood / Eucalyptus | Bleached Poplar / Mahogany | Must include ISPM 15 HT mark; test water resistance per batch |
| Inland Transport (Short-haul) | Class II (MUF) | Mixed Hardwood / Poplar | Mixed / Raw | Take rain protection measures; not for long-term outdoor storage |
| E-commerce Express Crates | Class III (UF) | Poplar | Raw | Cost priority, single use, no need to overemphasize water resistance |
| High-End Electronics Export | Class I (PF/WBP) + aluminum foil lamination | Birch / Eucalyptus | Bleached Poplar (clean appearance) | Must pair with desiccants and aluminum foil bag sealing for moisture protection |
VIII. Comparison of Packing Plywood with Other Packaging Materials
8.1 Comprehensive Performance Comparison
| Comparison Dimension | Packing Plywood | Solid Wood Crates | Corrugated Boxes | Plastic Returnable Crates (PP/PE) |
|---|---|---|---|---|
| Load Capacity | High (can bear >1000kg) | Very high (but affected by wood defects) | Low (<50kg, drops rapidly when wet) | Medium (100-300kg, but prone to aging and brittleness) |
| Impact Resistance | Excellent (multi-layer structure) | Excellent (but weak at knots) | Poor (almost no strength when wet) | Good (but brittle at low temperatures) |
| Moisture Resistance | Good (Class I up to waterproof) | Poor (naturally absorbs moisture, rots easily) | Very Poor (softens when wet) | Excellent (completely non-absorbent) |
| Weight (same volume) | Medium (approx. 600-750kg/m³) | Medium (approx. 500-700kg/m³) | Very light | Light (approx. 0.9-1.0g/cm³, but thinner walls) |
| Cost | Medium | Higher | Low | High (initial) |
| ISPM 15 Export Compliance | Built-in HT mark (fumigation-free) | Requires separate HT (added cost) | Exempt | Exempt |
| Environmental Impact | Low carbon (renewable, recyclable) | Low carbon (requires large-diameter logs) | Recyclable (but high production energy) | High carbon (petroleum-based, non-degradable) |
| Processing Flexibility | Excellent (saw, nail, drill, mill) | Excellent (same as plywood) | Easy to cut | Limited (requires injection/blow molding) |
| Single-Use Cost (100kg packaging example) | Low (approx. RMB 0.5-1.0/kg goods) | High (approx. RMB 1.0-2.0/kg) | Low (approx. RMB 0.2-0.5/kg, but only for light goods) | Medium (high initial, but reusable multiple times) |
8.2 Selection Recommendations — Match by Need
| Scenario | Preferred Material | Secondary Material | Justification |
|---|---|---|---|
| Export Heavy Cargo (>500kg) | Packing Plywood (Class I) | Solid Wood (with HT) | Lower cost, fumigation-free, moisture resistance better than solid wood |
| Export Light Cargo (<100kg, dry) | Corrugated Boxes (reinforced) | Thin Packing Plywood (3-6mm) | Lowest cost, but pay attention to moisture protection |
| High Humidity / Cold Chain | Packing Plywood (Class I + moisture-proof lamination) | Plastic Crates | Lower overall cost (plastic crates cost 3-5x more initially) |
| High Value / Precision Instruments | Packing Plywood (Class I, bleached face) + shockproof lining | Custom Plastic Crates | Sturdy, moisture-proof, clean appearance, good brand image |
| Single-Use Cheap Packaging | Thin Packing Plywood (Class III, 3-6mm) | Corrugated Boxes (heavy-duty) | Lowest cost with reliable strength |
IX. Technology Development Trends in Packing Plywood
9.1 Lightweighting and High-Strength Advancement
By optimizing veneer thickness (thinner but with more layers) and using high-strength species (increasing proportion of eucalyptus and birch), the unit area weight of packing plywood is reduced by 15-25% (from conventional 550-700kg/m³ to 450-550kg/m³) while maintaining equivalent strength. Lightweighting directly saves transport costs — for a 40-foot container (approx. 24-26 tons load), every 50-100kg weight reduction per cubic meter allows 5-8% more cargo.
Technical Approaches:
Increasing layer count (e.g., 5 layers instead of 3, 9 instead of 7) for higher strength in thinner veneers.
Using higher-density face veneers (okoume, eucalyptus) to improve surface hardness and impact resistance.
Optimizing lay-up configuration (increasing longitudinal veneer ratio) to enhance parallel-direction strength.
9.2 Environmental Protection & Circular Economy
Trend of PF Adhesive Replacing UF: Although PF adhesive costs more, its water resistance and environmental grades (can achieve E0 consistently) surpass UF, with formaldehyde-free raw materials. The proportion of PF adhesive in packing boards is rising from ~20% in 2020 to over 35% in 2025.
Recyclable/Degradable Packaging: Applying water-based biodegradable coatings on packing plywood surfaces as an alternative to traditional plastic moisture-proof films, allowing direct recycling after use (without separating plastic layers), simplifying the recycling process.
Circular Packaging Systems (Shared Pallets / Collapsible Returnable Crates): Collapsible returnable crates made from high-strength Class I packing plywood can achieve 50-100 cycles, with per-use costs far below single-use packaging. Widely adopted in Europe and North America, with rapid acceleration in China.
9.3 Intelligent & Digital Packaging
RFID Tag Embedding: Embedding RFID tags or NFC chips inside packing plywood (e.g., pallet decks) enabling end-to-end tracking of crates/pallets (from production, warehousing, transport to end customers), improving logistics transparency and inventory management efficiency.
Smart Sensor Integration: Pre-installing temperature-humidity sensors or vibration sensors inside packing boards (e.g., temperature loggers in cold chain transport) for real-time monitoring of transport environments, especially suitable for temperature/humidity-sensitive goods like precision instruments, pharmaceutical cold chain, and fresh produce.
Digital Packaging Design (CAD/CAE Optimization): Using Finite Element Analysis (FEA) for mechanical simulation of crate structures, optimizing board thickness, support structures, and connection methods — achieving minimal material usage while ensuring safety, saving 10-20% of packaging materials.
9.4 Surface Functionalization
Anti-Slip Treatment (Surface Embossing / Anti-Slip Coating): Embossing (diamond or striped patterns, depth 0.2-0.5mm) or applying anti-slip coatings (e.g., polyurethane anti-slip paint) to increase static friction during stacking, preventing slippage in multi-layer stacks.
Fire-Retardant Treatment: Adding phosphorus-nitrogen halogen-free flame retardants to raise fire rating from B2 to B1 (difficult to ignite), meeting fire safety requirements for dangerous goods packaging and special scenarios (chemicals, electronics warehousing).
Anti-Mold / Anti-Insect Treatment (Essential for Tropical Export Destinations): Adding boron-based or copper-azole (CuAz) preservatives to adhesives (Class I only) to resist mold and termite attack in tropical regions, extending crate service life in high-temperature high-humidity environments from 6 months to over 2 years.

JINDIWOOD · Engineered for Certainty — Every sheet of packing plywood is a steadfast guardian of industrial logistics safety and efficiency.
This article is an original technical publication by JINDIWOOD. Reproduction must indicate the source.